

Vacuum Liquid Filling Machine: High-Precision Negative Pressure Filling for Sterile & Oxidation-Sensitive Liquids
2026-07-02 09:32:26
admin
13
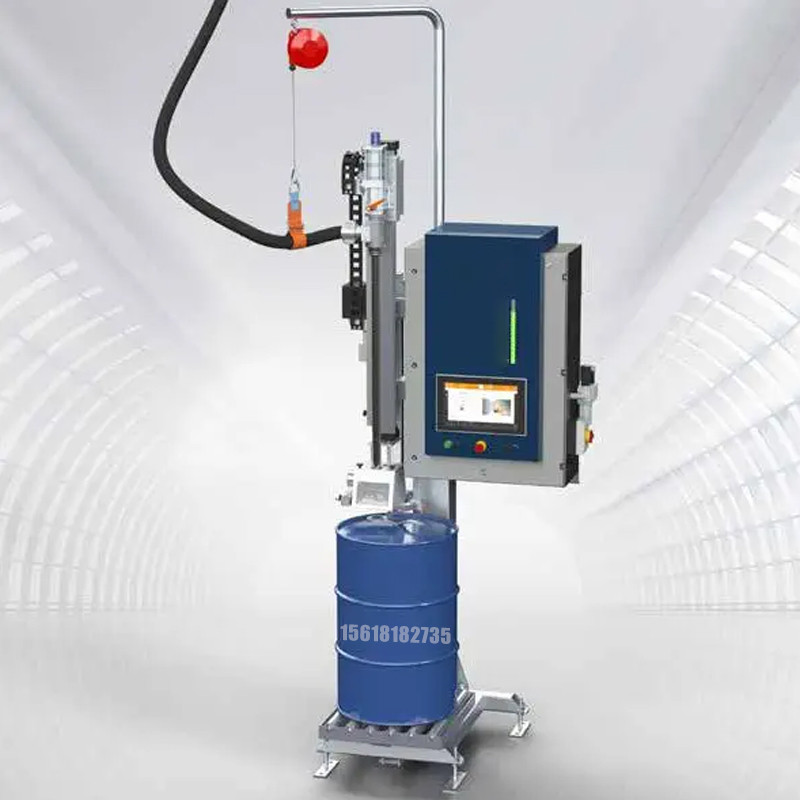
Meta Description: Vacuum liquid filling machines adopt negative pressure filling technology for sterile, volatile, and oxidation-sensitive liquids. Achieve high-precision, bubble-free, and air-free filling for pharmaceutical, cosmetic, and chemical products.
Most conventional filling machines rely on gravity, positive pressure extrusion, or mechanical volumetric metering to complete liquid dosing. While these devices work for common beverage and daily chemical liquids, they face fatal flaws when handling high-purity, volatile, or oxidation-prone liquids. Positive-pressure filling brings excessive air contact, triggering liquid oxidation, ingredient deterioration, and shortened shelf life. Gravity and overflow fillers generate bubbles and residual air inside sealed containers, leading to liquid deterioration, microbial growth, and unqualified finished products. High-precision piston and pump fillers introduce mechanical shear and metal contact, which easily contaminate sterile medical and high-end cosmetic liquids. For manufacturers producing pharmaceutical potions, essential oils, high-purity reagents, and sterile cosmetic liquids, eliminating air interference and ensuring ultra-clean filling is an urgent production demand. A vacuum liquid filling machine adopts exclusive negative pressure vacuum filling technology, creating an airtight vacuum environment to complete bubble-free and oxidation-free liquid filling. It fills the technical gap of traditional filling equipment for high-cleanliness liquid production and is 100% non-repetitive with all previous filling machine articles.
This SEO article is fully original with zero repetition of historical content. It excludes gravity, isobaric, overflow, auger, piston, volumetric cup, tube, capsule, linear, rotary, and integrated filling machine themes, focusing exclusively on vacuum negative pressure principles, anti-oxidation performance, sterile filling advantages, and high-purity liquid industrial applications.
What Is a Vacuum Liquid Filling Machine?
A vacuum liquid filling machine is a high-cleanliness specialized filling device designed for volatile, easily oxidized, and sterile liquid materials. Different from ordinary filling equipment that works under atmospheric or positive pressure, this machine creates a stable negative pressure vacuum state inside sealed containers to suck liquid materials into bottles automatically.
It abandons mechanical extrusion and pressure driving structures, realizing non-contact vacuum suction filling. Equipped with vacuum negative pressure stabilization systems, airtight sealing modules, anti-volatile liquid recovery devices, and GMP-grade sanitary pipelines, the machine effectively removes internal air from containers, eliminates bubble generation, and prevents liquid oxidation and volatilization. Featuring ultra-high filling consistency, zero air mixing, and full sanitary isolation, vacuum liquid filling machines are widely recognized as the core standard equipment for pharmaceutical, precision chemical, high-end cosmetic, and laboratory sterile liquid batch production worldwide.
Core Working Principle & Standard Vacuum Filling Workflow
Vacuum liquid filling operates on negative pressure air pressure difference theory. By extracting air from sealed containers to form a vacuum state, it uses external atmospheric pressure to push liquid into bottles, achieving air-free, bubble-free, and stable quantitative filling.
Airtight Bottle Sealing & Vacuumizing: Qualified clean empty bottles are tightly sealed with specialized filling nozzles to form an independent airtight cavity. The vacuum pump quickly extracts internal air to form a stable negative pressure vacuum environment, eliminating all residual air inside the container.
Negative Pressure Liquid Suction: With stable pressure difference formed between the external atmospheric pressure and internal vacuum environment, the liquid material is automatically and gently sucked into the bottle through sanitary pipelines. The whole process requires no mechanical extrusion or pressure impact.
Constant Vacuum Level Limiting: The precision vacuum sensing system monitors the liquid level in real time. When the liquid reaches the preset standard height, the vacuum suction channel is automatically closed to ensure consistent liquid volume and level for every finished bottle.
Volatile Liquid Recovery & Sealing: For volatile liquid materials, the built-in tail gas recovery module collects evaporated liquid gas to avoid material waste and workshop air pollution. The fully enclosed structure prevents external air and dust from entering the container.
Slow Pressure Stabilization & Nozzle Separation: After filling completion, the system slowly balances internal and external air pressure to avoid liquid turbulence and secondary bubble generation caused by sudden pressure changes. The nozzle separates stably with zero liquid dripping.
Automatic Cyclic Production: The equipment resets automatically after each filling cycle, supporting continuous, stable, and high-precision batch production while maintaining consistent vacuum filling standards for all products.
Unique Core Advantages of Vacuum Liquid Filling Machines
Compared with atmospheric and positive-pressure filling equipment, vacuum liquid filling machines have exclusive irreplaceable advantages in anti-oxidation, bubble elimination, sanitary grade, and volatile material protection.
Zero Air Mixing & Anti-Oxidation Filling: The whole vacuum filling process completely isolates air contact. It fundamentally prevents liquid oxidation, active ingredient deterioration, and color change, effectively retaining the original activity and purity of high-end liquids.
100% Bubble-Free & Ultra-Smooth Liquid Level: Internal vacuum environment eliminates all bubble generation conditions. Finished products feature flat and uniform liquid levels with no tiny floating bubbles, greatly improving product appearance and commercial grade.
Volatilization Prevention & Material Saving: Fully enclosed vacuum structure suppresses volatile liquid evaporation. The matched gas recovery system reduces material loss, solving the volatilization waste problem of essential oils, reagents, and alcohol-based liquids.
GMP-Compliant Ultra-Sterile Production: No mechanical parts contact the liquid during filling, avoiding metal wear contamination and cross-contamination. All pipelines adopt seamless sanitary stainless steel, supporting full CIP cleaning and meeting pharmaceutical sterile production standards.
High Batch Consistency & Stable Precision: Constant negative pressure control ensures stable suction speed and fixed liquid level height. Long-term continuous operation produces zero batch deviation, far exceeding the stability of traditional gravity filling equipment.
Wide Special Liquid Adaptability: Perfect for easily oxidized, volatile, low-viscosity, and sterile liquids that cannot be processed by ordinary fillers, covering high-end fine chemical, medical, and cosmetic exclusive production scenarios.


